
 EN
 English
 中文简体
Advanced DTY Yarn Solutions for Recycled, Functional, and High-Performance Textiles
Content
- 1 Understanding DTY Yarn and Its Role in Textile Production
- 2 A Broad Product Portfolio for Different Textile Requirements
- 3 Advantages Over Narrow or Standardized Yarn Suppliers
- 4 Advanced Manufacturing Process and Quality Control
- 5 R&D Strength and Application-Oriented Development
- 6 Applications of the DTY Product Range
- 7 How to Select the Correct DTY Specification
- 8 Customization and Customer Support
- 9 Environmental and Commercial Value
- 10 Frequently Asked Questions
- 10.1 What is the main advantage of DTY yarn?
- 10.2 What is the difference between SD DTY and FD DTY?
- 10.3 Why choose recycled DTY yarn?
- 10.4 What does the specification 75/72 mean?
- 10.5 What is cationic-dyeable DTY used for?
- 10.6 Is high-elastic DTY suitable for sportswear?
- 10.7 What are the benefits of PBT/PET yarn?
- 10.8 Where can moisture-wicking DTY be used?
- 10.9 Does antibacterial yarn remain effective after washing?
- 10.10 Can flame-retardant DTY guarantee that a finished garment is flame resistant?
- 10.11 Can the company develop a custom DTY specification?
- 10.12 What should be tested before placing a bulk order?
- 11 Conclusion
- 12 References
- 13 Product: General diagram of DTY except colored silk
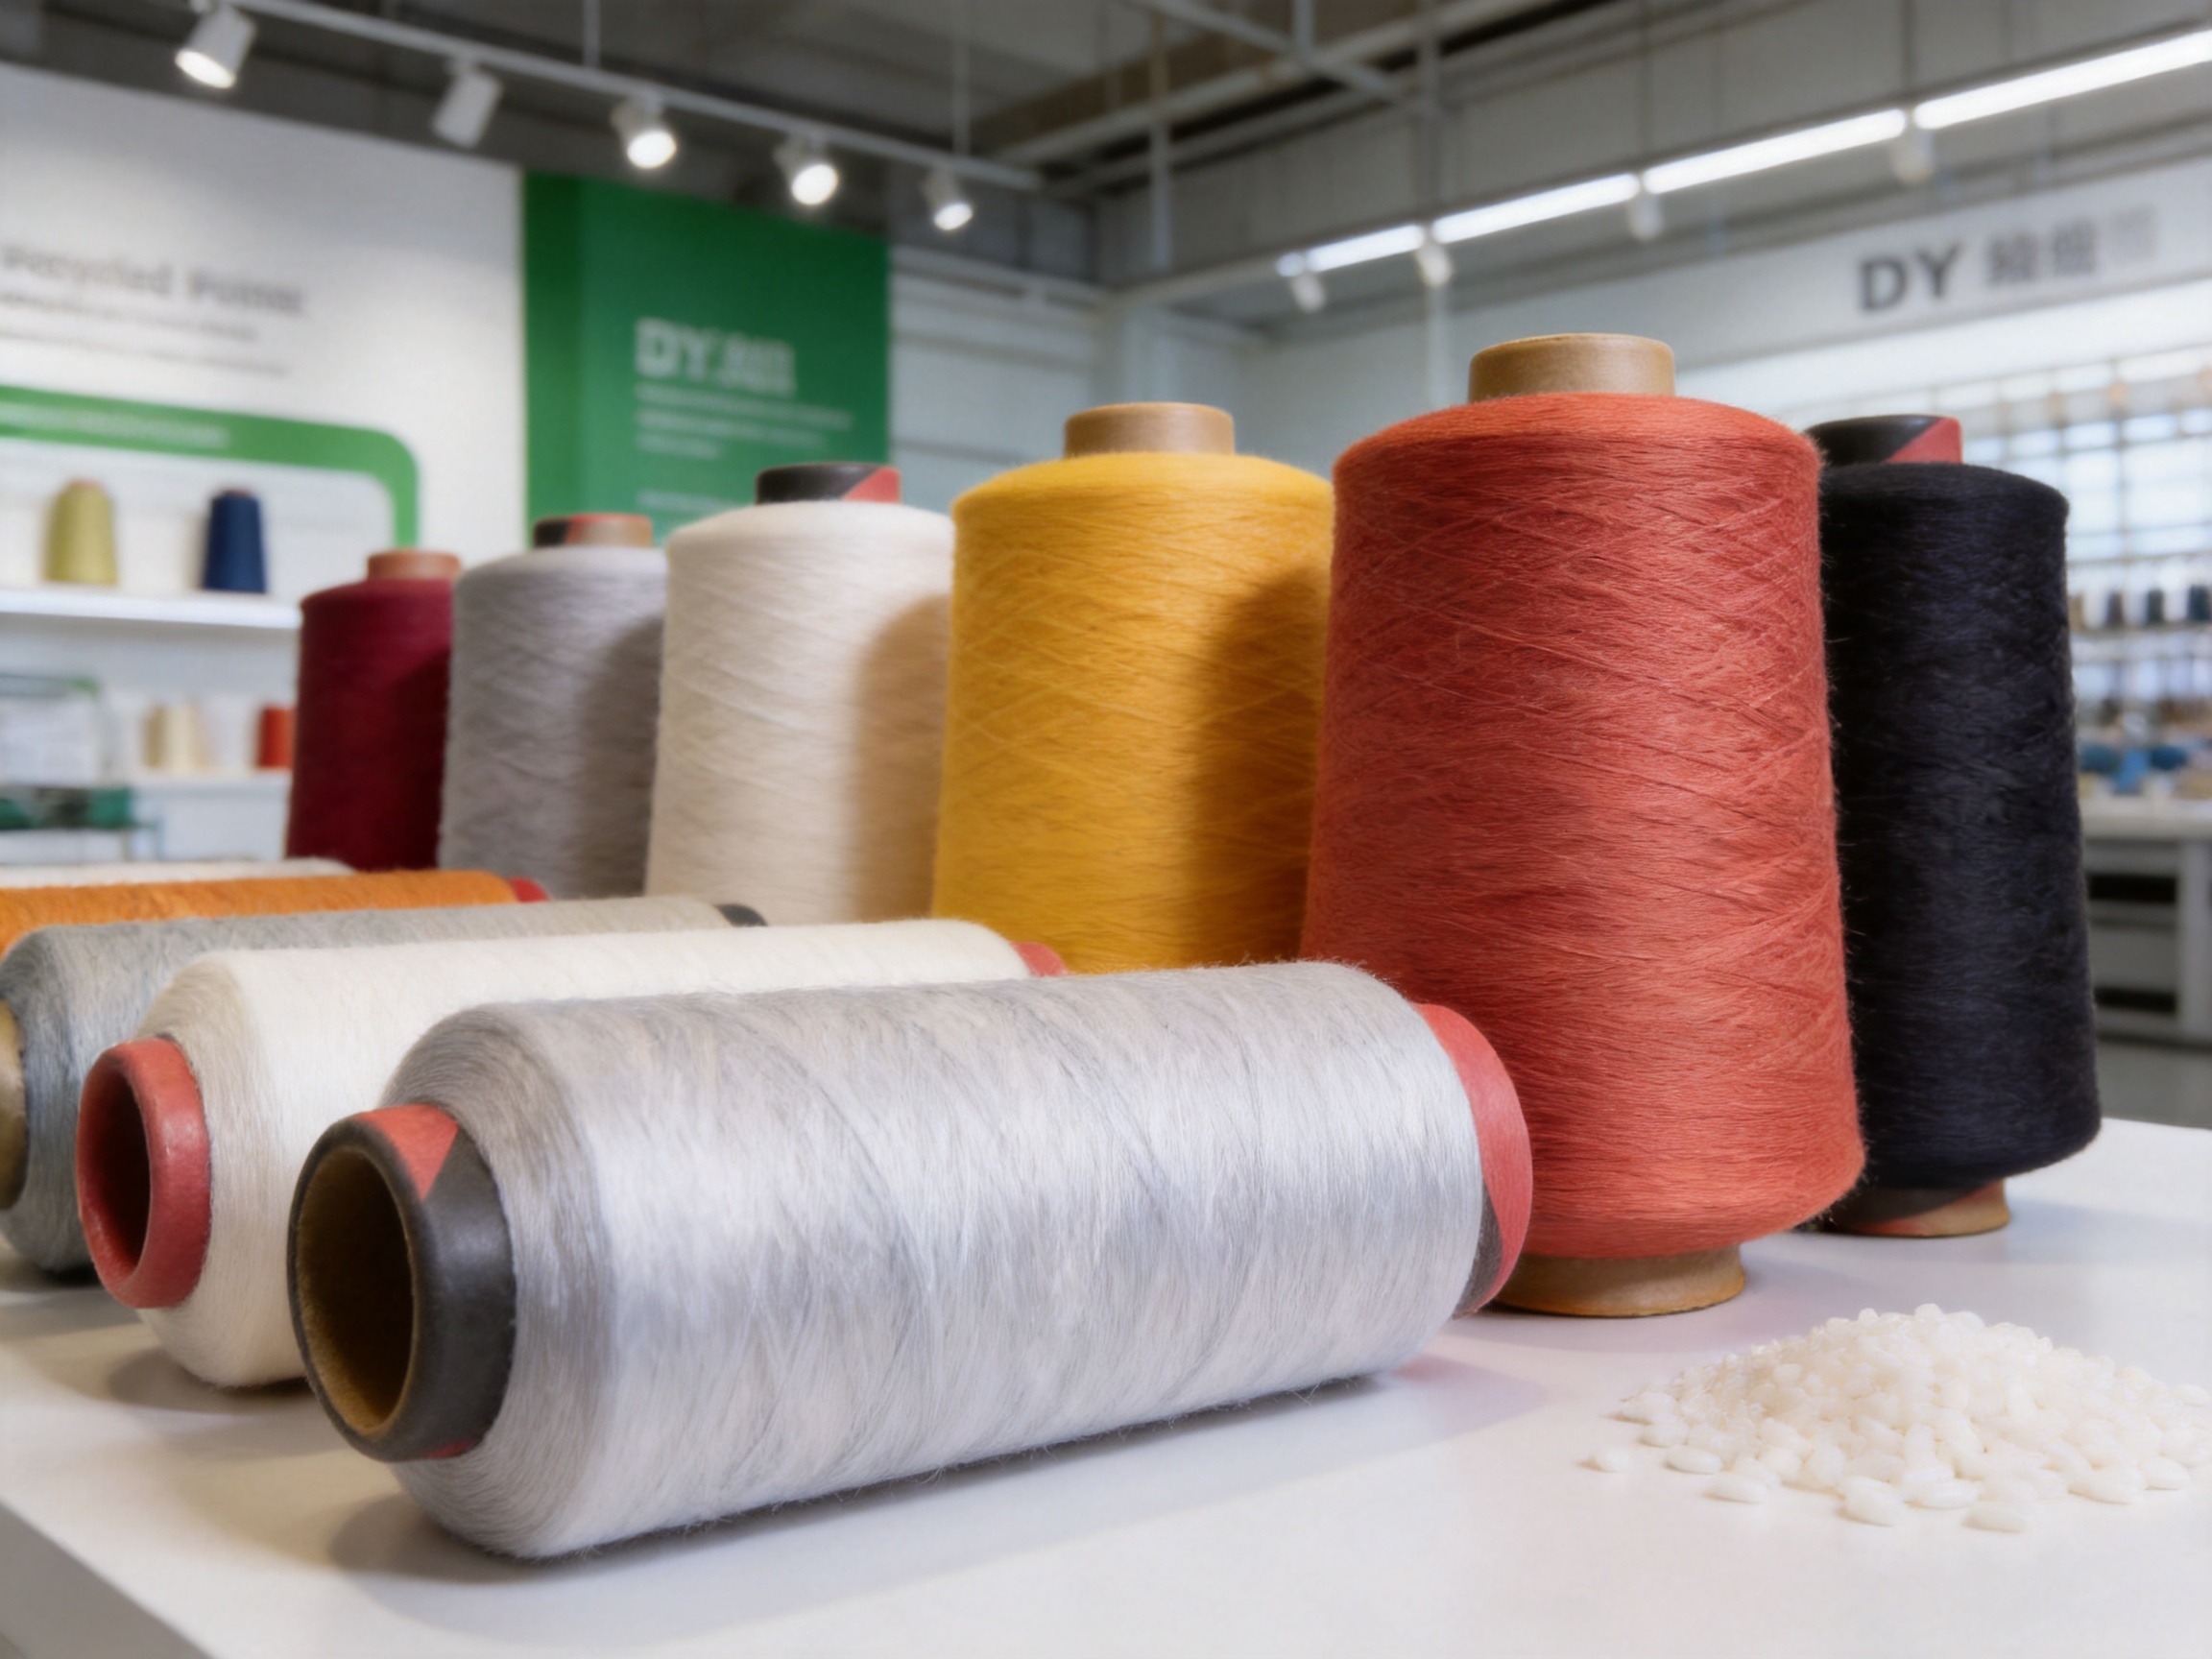
Draw textured yarn, commonly known as DTY yarn, is one of the most versatile materials used in modern textile manufacturing. It combines the strength and continuity of filament yarn with crimp, bulk, elasticity, softness, and visual character created through texturing. As a result, DTY yarn is widely used in knitted fabrics, woven fabrics, sportswear, casualwear, home textiles, upholstery, lingerie, activewear, and a wide range of technical textile applications.
The general product range presented by Suzhou Junhui Textile Co., Ltd. and Suzhou Xiaoran New Material Co., Ltd. is designed to serve buyers who require more than a standard polyester yarn. The range covers recycled DTY, normal polyester DTY, cationic-dyeable DTY, semi-dull and full-dull yarns, bright yarns, high-elastic yarns, PBT/PET composite yarns, functional yarns, hollow warm yarns, cotton-like yarns, and other differentiated products. This broad structure allows customers to select yarn according to fiber composition, luster, denier, filament count, elasticity, dyeing behavior, hand feel, and end-use requirements.
Compared with a narrow product portfolio based only on conventional polyester yarn, this product system offers greater flexibility for fabric developers, garment manufacturers, textile wholesalers, and brands searching for recycled and performance-oriented materials. It also gives customers the possibility of combining sustainable content with specialized functions, including moisture management, antibacterial properties, flame retardancy, cationic dyeing, and improved warmth.
The company’s product information includes numerous denier and filament combinations, such as 30/24, 50/72, 75/36, 100/144, 150/288, and 300/576. These specifications provide options for lightweight fabrics, medium-weight knitted structures, dense woven materials, brushed textiles, stretch fabrics, and decorative surfaces. The availability of both standard and customized differentiation yarns supports a development process in which yarn selection begins with the intended fabric performance rather than with a limited list of stock products.
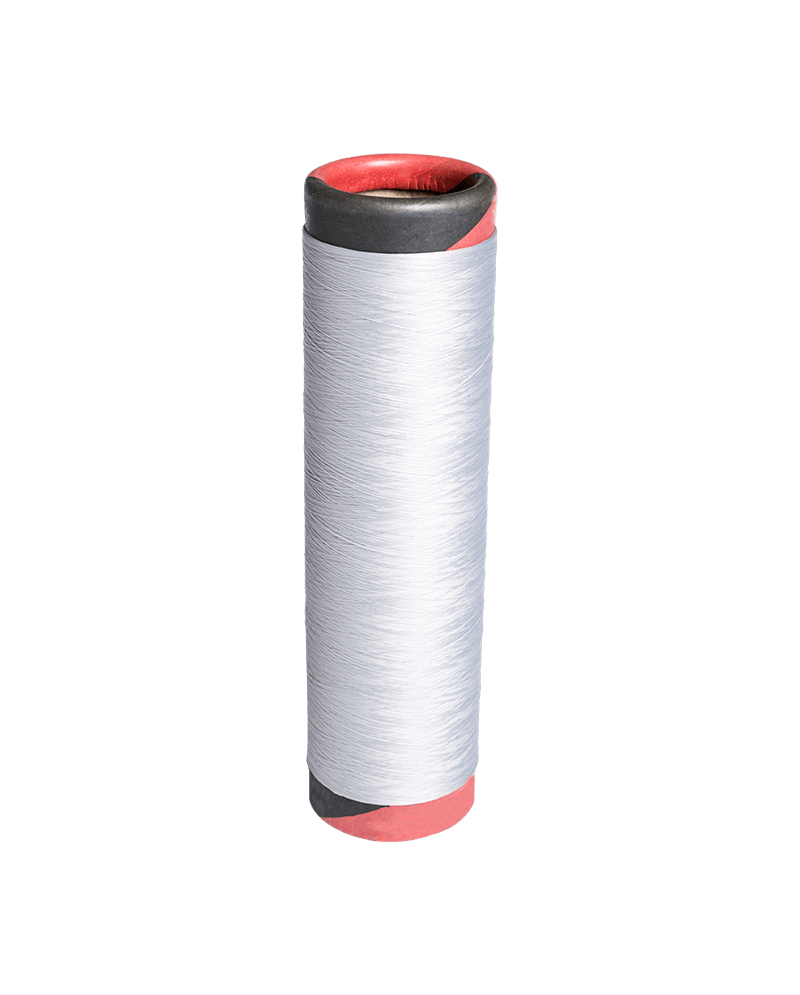
General diagram of DTY except colored silk
Understanding DTY Yarn and Its Role in Textile Production
DTY yarn is produced by applying heat, twisting, drawing, and mechanical texturing to partially oriented polyester yarn or another suitable filament feedstock. The texturing process creates a three-dimensional structure in the filament bundle. This structure increases bulk and gives the yarn a softer, more textile-like character than a completely flat filament yarn.
The exact performance of DTY depends on several variables. These include the polymer type, intrinsic viscosity, spinning quality, draw ratio, texturing temperature, false-twist conditions, winding tension, intermingling level, filament cross-section, luster, and final denier. A high-quality yarn must maintain consistent properties across the package and from lot to lot. If the crimp is uneven, the finished fabric may show streaks, barre, irregular dye uptake, or differences in surface appearance.
DTY is normally identified by denier and filament count. In a designation such as 75/72, the first number generally represents the total denier, while the second number represents the number of individual filaments. A 75-denier yarn with 72 filaments is relatively fine and can produce a smooth, soft, and compact surface. In comparison, a specification such as 150/144 contains more total mass and a high number of filaments, making it suitable for fabrics that require increased coverage, bulk, or a richer hand feel.
Denier and filament count should always be evaluated together. Two yarns with the same denier may behave differently if their filament counts are different. A higher filament count generally provides finer individual filaments, which can improve softness and surface smoothness. A lower filament count may create a more pronounced texture or a different visual effect. This is why a diversified product range is valuable to textile mills: it allows the yarn to be selected according to the construction and finishing method of the target fabric.
Important DTY Yarn Characteristics
The most important characteristics of DTY yarn include tensile strength, elongation, crimp contraction, crimp stability, boiling water shrinkage, evenness, oil content, intermingling, winding quality, and dye uniformity. These properties influence knitting efficiency, weaving performance, fabric recovery, dimensional stability, and the appearance of the final product.
For knitted fabrics, yarn must run smoothly through feeders and guides while maintaining stable tension. Excessive hairiness, broken filaments, poor package formation, or inconsistent intermingling can lead to needle lines, dropped stitches, holes, and fabric defects. For woven fabrics, the yarn must also withstand the mechanical stress of warping, sizing, and weaving. A stable DTY package helps reduce production stoppages and improves the consistency of the greige fabric.
Texturing also affects the tactile identity of the fabric. A soft, bulky DTY may be ideal for underwear, sportswear, fleece, and comfortable casual garments. A more stable and compact yarn may be better for smooth woven fabrics or apparel linings. Semi-dull, full-dull, and bright options can further change the visual effect, ranging from a subdued matte appearance to a clean and reflective surface.
A Broad Product Portfolio for Different Textile Requirements
The presented product list is organized into several series. Each series is intended to solve a different combination of cost, performance, sustainability, appearance, and processing requirements. This segmentation makes it easier for customers to identify an appropriate starting point for product development.
Recycled DTY Yarn Series
The recycled series includes recycled semi-dull DTY, recycled full-dull DTY, recycled semi-dull and cationic-dyeable DTY, recycled DDB DTY, and recycled cationic-dyeable DTY. The listed specifications include 15/6, 20/12-24, 30/12-24-36, 50/36-48-72, 75/36-72-144, 100/36-48-96-144, 150/48-96-144-288, and 300/96-192-288-576 for selected recycled products.
Recycled polyester yarn helps textile manufacturers reduce their reliance on virgin polyester feedstock. It can support sustainability programs, recycled-content targets, and product lines that respond to growing consumer interest in circular materials. However, recycled yarn must still meet practical production requirements. It needs suitable strength, stable elongation, reliable texturing performance, and consistent dyeing behavior. A recycled label alone is not enough if the yarn causes high breakage or unstable fabric quality.
The strength of a well-developed recycled DTY range is that sustainability is integrated with usable textile performance. Customers can choose different luster levels, filament counts, and deniers rather than accepting a single recycled specification for every application. Recycled semi-dull yarn may be suitable for everyday knitwear, while recycled full-dull yarn can provide a softer and more subdued surface. Recycled cationic-dyeable yarn offers additional design possibilities where contrasting dye effects or specialized coloration are required.
Normal Polyester DTY Series
The normal series includes semi-dull DTY, full-dull DTY, and semi-dull DDB products. The available specifications cover a broad range, including 25/72, 30/12-24-36-72, 50/36-48-72-144, 75/36-48-72-144, 100/36-48-96-144, 120/144, 150/48-96-144-288, 200/96-288-384, and 300/96-192-288-576.
Conventional polyester DTY remains important because it offers a reliable balance of strength, durability, processability, and price. It is used in sportswear, knitted garments, fashion fabrics, linings, home textiles, blankets, curtains, and many other products. The normal series can serve customers that prioritize stable production, broad availability, and predictable performance.
Semi-dull and full-dull variants provide different surface effects. Semi-dull yarn produces a controlled and moderately subdued appearance. Full-dull yarn contains a higher level of delustering and is often selected for a softer visual effect with reduced shine. DDB yarns can be used when the customer needs a particular combination of texture and appearance. By offering multiple luster choices, the product range helps fabric mills match yarn selection with the intended design language of the finished textile.
Cationic-Dyeable DTY and CD Series
The CD series includes cationic-dyeable DTY, semi-dull and cationic-dyeable DTY, and white and black yarn products. Listed cationic-dyeable options include 25/24, 30/24-36, 50/36-72, 75/36-72-144, 100/36-48-72-144, 150/48-144-288, and 300/96.
Cationic-dyeable polyester is valued for its ability to create distinctive coloration effects. In blended or combined constructions, cationic-dyeable yarn can be dyed differently from conventional polyester, producing two-tone, heathered, mélange, contrast, or shadow effects. This makes it useful for fashion fabrics and designs that require visual depth without relying only on printing or complex finishing.
The availability of white and black yarn in specifications such as 100D B01/B02/B03 and 150D B01/B02/B03 provides additional options for designers and fabric mills. The exact code may represent internal color or construction classifications, so customers should confirm technical details before production. Nevertheless, the presence of these options demonstrates an emphasis on differentiated yarn rather than a single standard product.
High-Elastic and PBT/PET Yarn
The high-elastic series includes high-elastic yarn, PBT/PET yarn, and PBT/PET DDB yarn. The listed high-elastic specifications include 30/12, 50/36-72, 60/72, 75/36-72, and 150/48-144. PBT/PET products include 50/48 and 75/36, while high-elastic combination specifications include SD/FD 30/24, 50/36-48-72, 75/36-48-72, 150/72-144, and 300/96-144.
Elasticity is a major requirement in sportswear, leggings, fitted garments, swimwear, socks, underwear, and stretch knit fabrics. High-elastic DTY can provide controlled stretch and recovery while maintaining the familiar processing advantages of a filament yarn. PBT/PET constructions can be selected when the product developer wants a particular balance of elasticity, resilience, dimensional stability, and dyeing behavior.
Compared with an ordinary polyester yarn, a well-designed elastic yarn can reduce the need for additional elastic components in some fabric constructions. This may simplify production and contribute to a cleaner fabric structure. The correct choice depends on the target stretch percentage, recovery requirement, fabric construction, finishing method, and garment pattern. Technical sampling is recommended because the same yarn can perform differently in single jersey, interlock, rib, warp knit, or woven structures.
Functional DTY Yarn Series
The functional series includes flame-retardant yarn, antibacterial yarn, moisture-wicking yarn, cotton-like yarn, hollow warm yarn, and Acy yarn. These products are intended to give textile manufacturers greater freedom to develop fabrics with a specific comfort, safety, or appearance benefit.
Flame-retardant yarn is listed in semi-dull and full-dull options, including SD/FD 75/36-72 and SD/FD 150/36-48-144. Such yarn may be used for workwear, protective clothing, transportation interiors, hospitality textiles, and other applications where flame performance is part of the product specification. Flame-retardant performance must always be validated according to the applicable fabric construction, finishing process, and market standard. A yarn description alone does not guarantee that a finished fabric will meet a particular regulation.
Antibacterial DTY is listed in 50/48-72, 75/36-48-72, and 150/48-72-96-144. It may be considered for sportswear, socks, underwear, bedding, medical-related textiles, and other products where odor control or microbial management is important. The final performance depends on the active technology, concentration, migration behavior, washing durability, fabric structure, and testing method. Customers should request technical documentation and test reports appropriate to the intended application.
Moisture-wicking yarn is listed in 30/24, 50/48-72, 75/48-72, and 150/48-72. Moisture management can be created through polymer modification, filament cross-section, capillary structure, yarn texturing, or a combination of these factors. Moisture-wicking DTY is especially suitable for athletic apparel, base layers, travel clothing, uniforms, and warm-weather garments. The fabric design remains important because knitting density, finishing, and garment construction all influence drying speed and perceived comfort.
Cotton-Like, Hollow Warm, and Acy Yarn
Cotton-like products are listed as 32S, 40S, and 80S. These yarns are developed to imitate selected characteristics of spun cotton yarn, including a softer hand, a more natural appearance, and a less synthetic surface impression. Cotton-like filament yarn can provide the visual and tactile benefits of a cotton-inspired fabric while retaining the continuity and production efficiency of filament yarn.
Hollow warm yarn is available in 75/72 and 150/144. Hollow structures can trap air within or around the filament bundle, helping to create a lighter and warmer textile effect. These yarns may be considered for thermal underwear, winter sportswear, sweaters, blankets, and other products where warmth and low weight are desirable. Actual insulation depends on yarn structure, fabric thickness, loft, brushing, garment design, and air permeability.
Acy yarn options include 40+75/36-72, 30+100/96, and 40+150/48-96-144. These specifications indicate combined components designed to create a differentiated appearance or hand feel. Acy yarn can be useful for mixed-effect fabrics, textured surfaces, and products that require a more complex visual or tactile result than a single-component yarn can provide.
Product series | Representative products | Typical development value |
Recycled series | Recycled SD DTY, recycled FD DTY, recycled SD+CD DTY, recycled CD DTY | Supports recycled-content programs and sustainable product development |
Normal series | SD DTY, FD DTY, SD DDB | Reliable performance for general knitting and weaving applications |
CD series | CD DTY, SD+CD DTY, white and black yarn | Creates differentiated dyeing and visual effects |
High-elastic series | High-elastic yarn, PBT/PET, PBT/PET DDB | Supports stretch, recovery, comfort, and body-conforming fabrics |
Functional series | Flame-retardant, antibacterial, moisture-wicking | Adds comfort, safety, hygiene, or performance characteristics |
Special hand-feel series | Cotton-like, hollow warm, Acy | Provides softness, warmth, bulk, and differentiated surface effects |
Advantages Over Narrow or Standardized Yarn Suppliers
One of the principal advantages of this product range is breadth. Many textile suppliers focus on a small selection of conventional DTY specifications. That approach may work for basic production, but it can restrict fabric innovation. A customer developing sustainable sportswear, for example, may need recycled content, moisture management, elasticity, and a specific matte appearance at the same time. A supplier that offers only standard semi-dull polyester may not be able to provide an efficient solution.
The range described here gives buyers access to several dimensions of product differentiation. They can compare recycled and conventional feedstocks, choose between semi-dull and full-dull effects, select standard or cationic-dyeable structures, and evaluate high-elastic or functional options. This creates a more efficient development pathway and reduces the need to coordinate with multiple suppliers for closely related products.
Another advantage is the wide denier and filament-count coverage. Fine specifications can be used for lightweight and soft fabrics, while heavier specifications can provide coverage, warmth, and durability. Multiple filament counts within similar denier ranges allow customers to fine-tune softness, bulk, surface smoothness, and fabric appearance.
The product list also demonstrates an ability to support both mainstream and niche requirements. Normal SD DTY and FD DTY can serve high-volume applications, while recycled, antibacterial, flame-retardant, moisture-wicking, cationic-dyeable, and high-elastic products serve more specialized markets. This balance is commercially important because textile customers often need a supplier that can support their basic volume programs while also helping them develop higher-value products.
A further advantage is the stated willingness to accept orders for different kinds of differentiated yarn. Custom development is particularly valuable when the customer has a fabric target but no existing yarn specification. Instead of selecting a product only from a fixed catalog, the customer can discuss denier, filament count, luster, elasticity, dyeing behavior, function, and end use with the supplier’s technical team.
Advanced Manufacturing Process and Quality Control
The quality of DTY yarn is determined by the entire manufacturing chain, beginning with polymer and feedstock preparation and continuing through spinning, texturing, winding, inspection, packaging, and shipment. A strong manufacturer must control not only the final yarn but also the conditions that create its properties.
Feedstock Preparation and Polymer Consistency
For polyester yarn, the condition of the polymer or recycled feedstock directly affects spinning stability and final yarn performance. Moisture control is essential because excessive moisture can cause hydrolytic degradation during melting and reduce the strength or viscosity of the polymer. Feedstock should therefore be handled, stored, and dried under controlled conditions appropriate to the material.
Recycled materials may require additional preparation because the feedstock can vary in origin, color, contamination level, and molecular history. Effective sorting, cleaning, filtration, and quality assessment help improve melt stability. A controlled recycled-material process is essential for producing yarn with consistent denier, color, strength, and dyeing behavior.
For differentiated yarns, the feedstock may also contain additives or modified polymer components. These can be used to create cationic dyeability, flame retardancy, antibacterial properties, special luster, or other functions. The formulation must be balanced carefully so that the desired function does not create excessive brittleness, poor spinnability, unstable color, or reduced texturing performance.
Melt Spinning and Filament Formation
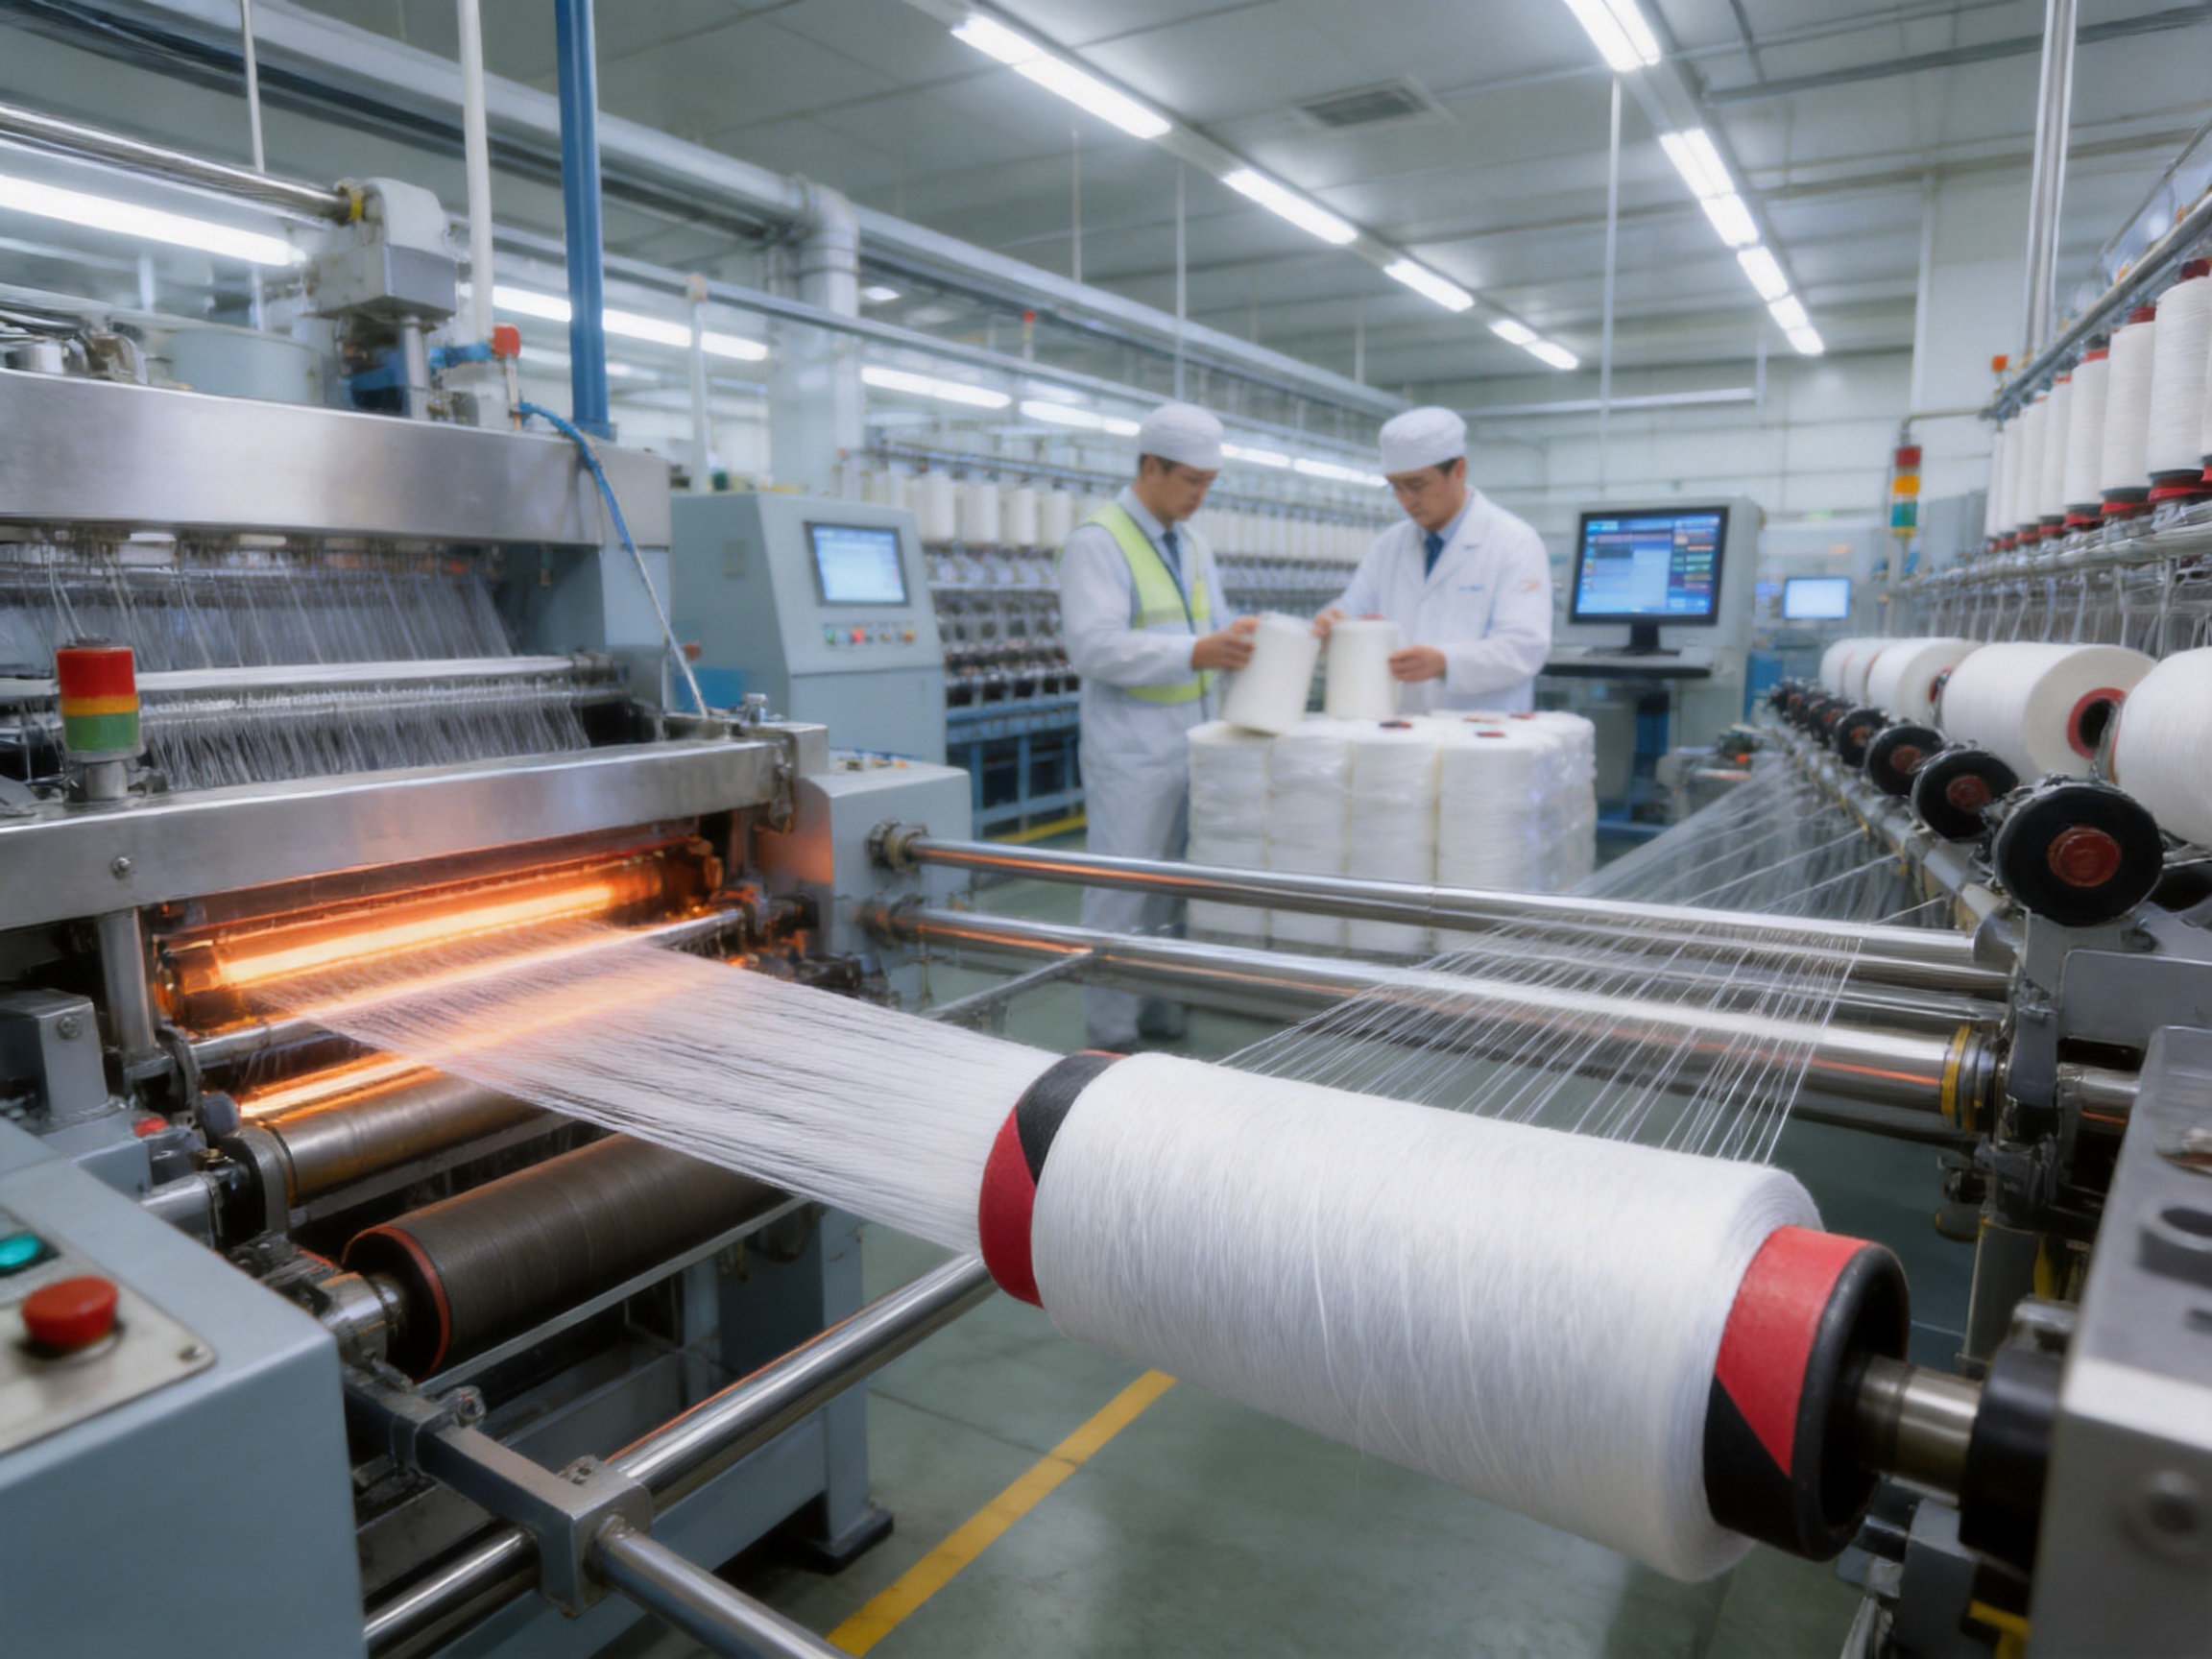
During melt spinning, polymer is melted and metered through a spinneret to form continuous filaments. Temperature, pressure, throughput, cooling air, and take-up speed must be controlled to create a stable filament bundle. Spinneret design influences filament count, cross-section, and uniformity. The cooling process affects crystallization, orientation, and the behavior of the resulting partially oriented yarn.
Uniform filament formation is particularly important for DTY because the texturing machine processes many individual filaments simultaneously. If some filaments have different denier, orientation, or thermal history, the final yarn may exhibit uneven crimp or irregular dye uptake. Stable spinning conditions therefore support better texturing consistency later in the process.
Online monitoring and laboratory testing can be used to verify denier, evenness, strength, elongation, and appearance. Production teams may also monitor pressure changes, spinneret condition, winding tension, and package formation. Early detection of process variation helps reduce the risk of producing large quantities of nonconforming yarn.
Drawing and False-Twist Texturing
DTY production generally uses a drawing and false-twist texturing process. The feed yarn is drawn to develop the desired molecular orientation and then heated so that the filaments can be shaped. False twist temporarily twists the filament bundle, allowing the individual filaments to form crimp when the yarn is untwisted and cooled.
Important texturing parameters include heater temperature, draw ratio, spindle speed, overfeed, twisting conditions, cooling conditions, friction-disc arrangement, and yarn tension. These variables influence bulk, stretch, recovery, crimp stability, and hand feel. A supplier with experience across recycled, standard, elastic, and functional yarns must be able to adjust these parameters to the characteristics of each material.
Recycled feedstock can require careful optimization because its thermal response may differ from that of virgin polymer. Functional additives can also influence friction, heat transfer, elongation, and filament strength. PBT/PET and other composite constructions require precise control so that the components develop the intended relationship during heating and cooling.
Texturing is not simply a mechanical step. It is a controlled transformation of a flat filament bundle into a yarn with a specific three-dimensional structure. When the conditions are stable, the yarn can provide consistent bulk and elasticity. When the conditions vary, the fabric may show differences in stretch, recovery, density, and surface appearance. This is why advanced equipment must be combined with experienced process management.
Intermingling and Winding
Intermingling helps improve the cohesion of the filaments. It can reduce filament separation during downstream processing and support smoother knitting or weaving. The correct level of intermingling depends on the yarn type and application. Too little cohesion may result in opening, snagging, or unstable processing, while excessive intermingling may influence softness and fabric appearance.
Winding quality is another critical factor. A yarn package must have a stable shape, appropriate hardness, and uniform density. Poor winding can lead to tension fluctuations, yarn sloughing, unwinding problems, and machine stoppages at the customer’s facility. A well-formed package supports efficient transport, storage, and downstream use.
For export-oriented production, packaging must also protect the yarn from moisture, contamination, compression, and handling damage. Clear identification of product name, specification, lot number, package number, and production information helps customers maintain traceability and inventory control.
Testing and Inspection
A professional DTY quality system normally includes tests for linear density, tensile strength, elongation, crimp contraction, crimp stability, shrinkage, oil content, intermingling, evenness, and visual defects. The precise test program should be matched to the product and customer requirements.
For functional yarns, additional tests are needed. Antibacterial yarn may require microbial reduction testing and durability assessment. Flame-retardant yarn requires testing under the relevant standard and, in many cases, evaluation after washing. Moisture-wicking yarn should be assessed using an appropriate moisture transport method. Recycled products may require documentation concerning recycled content and chain-of-custody procedures where relevant.
The company’s stated focus on research and development, international cooperation, and application support is important in this context. Textile performance is ultimately judged at the fabric and garment level. A yarn supplier that understands knitting, weaving, dyeing, and finishing can provide more useful technical recommendations than one that only sells a specification sheet.
R&D Strength and Application-Oriented Development
Suzhou Junhui Textile Co., Ltd. and Suzhou Xiaoran New Material Co., Ltd. were established in June 2015 and are described as enterprises focused on differentiated yarn, recycled yarn, polyester dope-dyed yarn, SHAWLIENCE, microfine yarn, flame-retardant yarn, cationic-dyeing yarn, and knitting fabric products. Their stated R&D activity includes cooperation with internationally recognized enterprises in environmental protection and functional yarn and fabric development.
This application-oriented approach is valuable because the most suitable DTY yarn is rarely selected by denier alone. A fabric designer may need a soft hand, a matte surface, controlled stretch, rapid moisture spreading, or a specific dye contrast. Each requirement can affect the choice of polymer, filament count, luster, texturing condition, and finishing route.
For example, a customer developing recycled sportswear may need to balance four goals: recycled content, moisture management, elasticity, and color fastness. A product developer working on winter knitwear may prioritize hollow warmth, bulk, softness, and low weight. A fashion fabric designer may want a cationic-dyeable yarn combined with a conventional polyester yarn to produce a two-tone effect. These projects require technical communication across several stages rather than a simple purchase transaction.
The company’s broad export customer base, described as covering 36 countries, also indicates experience with international product requirements and communication. Export-oriented customers often expect stable documentation, consistent packaging, predictable lead times, and support with product selection. A supplier that can communicate effectively across markets is better positioned to support long-term development programs.
Applications of the DTY Product Range
Sportswear and Activewear
Sportswear requires a combination of stretch, recovery, moisture management, softness, and durability. High-elastic DTY and PBT/PET yarns can help create fabrics that move with the body. Moisture-wicking yarn can assist in spreading perspiration across the fabric surface, where it may evaporate more efficiently. Recycled versions can support activewear collections positioned around lower environmental impact.
The final result depends on knitting structure, fabric weight, finishing, and garment design. Yarn selection should therefore be tested in the intended fabric construction. A lightweight single jersey may require a different specification from a compact interlock or a heavy tricot fabric.
Casualwear and Fashion Fabrics
DTY yarn is widely used for T-shirts, dresses, skirts, trousers, jackets, and fashion knitwear. Semi-dull and full-dull yarns can create different levels of visual softness, while cationic-dyeable yarn can provide contrast effects and richer color dimensions. Cotton-like products may be useful for garments that need a more natural hand feel while retaining filament-yarn processing advantages.
Acy and other differentiated yarns can add texture or visual complexity to fashion fabrics. By selecting the appropriate denier and filament count, fabric developers can create smooth surfaces, brushed effects, compact structures, or bulky constructions.
Home Textiles
DTY is suitable for bedding, blankets, curtains, upholstery, cushions, and decorative fabrics. Heavier denier options can provide coverage and durability, while hollow warm yarn can support lightweight thermal products. Full-dull yarn may be selected for a calm and subdued interior appearance, whereas brighter yarn can create a cleaner and more reflective surface.
For home textiles, dimensional stability, washing durability, color consistency, and resistance to pilling are important considerations. Yarn selection should be coordinated with fabric construction and finishing. For products exposed to sunlight, heat, or repeated laundering, the full textile system should be evaluated rather than relying on yarn data alone.
Workwear and Technical Clothing
Flame-retardant yarn can be considered for uniforms, protective garments, industrial clothing, transportation-related textiles, and other applications where fire behavior is a central requirement. The final garment must be tested according to the applicable standard because flame performance depends on yarn content, fabric weight, construction, seams, finishes, and laundering.
Antibacterial yarn may also be used in uniforms, hospitality textiles, healthcare-related products, and garments requiring improved odor management. Again, product claims should be supported by appropriate test evidence and should be communicated accurately to end users.
Knitting and Weaving Production
The range is suitable for both knitting and weaving applications. Knitters may select fine filament products for soft and lightweight structures or higher-denier yarns for coverage and bulk. Weavers may use DTY for warp or weft applications, depending on the required construction and processing conditions.
Before bulk purchasing, mills should conduct trials that examine yarn tension, machine speed, needle or heddle behavior, breakage rate, fabric appearance, dye uptake, and finishing response. A technically suitable yarn should also be commercially practical, with stable package quality and dependable lot consistency.
How to Select the Correct DTY Specification
The first step is to define the finished textile rather than choosing yarn in isolation. The buyer should identify the fabric type, target weight, stretch requirement, hand feel, luster, color effect, performance claims, and expected care conditions.
The second step is to select the material platform. Conventional polyester may be suitable for cost-efficient general production. Recycled polyester may be preferred for sustainability objectives. Cationic-dyeable yarn may be needed for contrast effects. PBT/PET or high-elastic yarn may be appropriate for stretch and recovery. Functional yarn should be selected only when its specific performance is required and can be verified.
The third step is to determine denier and filament count. Fine denier yarns generally support lightweight and soft fabrics, while heavier yarns provide more coverage and body. Higher filament counts can contribute to a finer and softer surface. The relationship between denier, filament count, and fabric construction should be confirmed through sample knitting or weaving.
The fourth step is to define luster. Semi-dull yarn offers a controlled appearance with moderate reflection. Full-dull yarn gives a more subdued look. Bright yarn can create a cleaner and more reflective effect. Luster selection affects not only the yarn itself but also the perceived depth and saturation of dyed fabric.
The fifth step is to evaluate functional requirements and compliance. If the product is marketed as recycled, antibacterial, moisture-wicking, or flame-retardant, the buyer should request relevant documentation. Test methods, standards, durability, and claim language should be agreed before mass production.
The final step is to conduct a complete trial. The sample should be processed under conditions similar to bulk production. Testing should include knitting or weaving efficiency, dyeing, finishing, washing, dimensional stability, pilling, color fastness, and appearance. This process helps prevent problems that cannot be identified from a yarn sample alone.
Selection factor | Questions for the buyer | Possible product direction |
Sustainability | Is recycled content required or preferred? | Recycled SD, recycled FD, recycled CD, or recycled SD+CD DTY |
Surface appearance | Should the fabric be matte, subdued, or more reflective? | Full-dull, semi-dull, or bright-related option |
Stretch | What stretch and recovery are required? | High-elastic or PBT/PET yarn |
Dyeing effect | Is contrast or two-tone coloration desired? | Cationic-dyeable or SD+CD DTY |
Comfort | Is softness, warmth, or moisture control important? | Cotton-like, hollow warm, or moisture-wicking DTY |
Safety or hygiene | Is flame behavior or antibacterial performance required? | Flame-retardant or antibacterial DTY |
Fabric weight | Is the target fabric lightweight, medium, or heavy? | Select denier and filament count accordingly |
Customization and Customer Support
The company states that it can accept orders for different kinds of differentiated yarn. This is significant for customers whose requirements do not match a standard catalog item. Customization may involve denier, filament count, luster, recycled content, cationic-dyeable behavior, elastic response, functional additives, or a combination of several characteristics.
A successful custom project should begin with a clear technical brief. The buyer should provide the end use, fabric construction, target weight, target stretch, dyeing method, finishing process, performance claims, certification needs, and anticipated order quantity. The supplier can then recommend a suitable development route and identify the specifications that require sampling.
Technical support is especially important for differentiated yarn because changes in one property can influence others. Increasing elasticity may affect dimensional stability. Adding a functional component may change dyeing behavior. Increasing luster control may influence softness or color appearance. Recycled content may require adjustments to texturing conditions. Experienced development teams can help identify these relationships before bulk production.
The company’s stated commitment to responding to professional guidance and product-selection requests within 12 hours globally also supports international cooperation. Fast communication does not replace technical accuracy, but it can shorten the time required to clarify specifications, arrange samples, discuss test results, and solve production questions.
Environmental and Commercial Value
The recycled series addresses one of the most important trends in the textile industry: the shift toward lower-impact materials and more traceable supply chains. Recycled polyester can help reduce dependence on virgin resources and provide a pathway for using recovered material in new textile products. Its suitability must be verified through quality testing and, where required, recognized certification systems.
Environmental value also depends on product durability. A fabric that lasts longer, retains its appearance, and remains functional through repeated washing may deliver greater practical value than a material that has recycled content but poor service life. Consistent DTY quality therefore contributes to sustainability by reducing production waste, improving manufacturing efficiency, and supporting longer-lasting products.
Functional yarns can also contribute to resource efficiency. Moisture-wicking materials may improve comfort and reduce the need for heavy fabric treatments. Durable antibacterial performance may support longer use in selected applications. High-elastic yarn can help create garments that retain shape, while hollow warm yarn may provide thermal comfort with lower material weight. These benefits should be evaluated through the entire life cycle and supported by accurate product claims.
Commercially, a broad differentiated-yarn range allows manufacturers to move beyond price-only competition. Recycled, functional, and specialty fabrics can support higher-value product categories and help brands respond to changing consumer expectations. Suppliers that combine manufacturing capacity with R&D support are better positioned to participate in this transition.
Frequently Asked Questions
What is the main advantage of DTY yarn?
DTY yarn combines continuous-filament strength with textured bulk, softness, stretch, and a more textile-like hand feel. It can be used in both knitted and woven fabrics and is available in many denier, filament-count, and luster combinations.
What is the difference between SD DTY and FD DTY?
SD generally refers to semi-dull yarn, which has a controlled and moderately subdued appearance. FD generally refers to full-dull yarn, which has a stronger delustered effect and a softer visual impression. The appropriate choice depends on the desired fabric appearance and end use.
Why choose recycled DTY yarn?
Recycled DTY can help textile manufacturers incorporate recycled polyester into their products and reduce reliance on virgin polyester feedstock. It is suitable for sustainability-focused apparel, home textiles, and other products, provided that the yarn meets the required strength, consistency, dyeing, and certification standards.
What does the specification 75/72 mean?
In common textile notation, 75 usually refers to the total denier and 72 refers to the number of filaments. The exact interpretation should be confirmed with the supplier’s technical data sheet, especially for special or composite products.
What is cationic-dyeable DTY used for?
Cationic-dyeable DTY is used to create special coloration effects, including two-tone, contrast, mélange, and shadow effects. It can be combined with conventional polyester yarns in selected fabric constructions to produce differentiated visual results.
Is high-elastic DTY suitable for sportswear?
High-elastic DTY can be suitable for sportswear, leggings, fitted garments, underwear, and other stretch products. The final stretch and recovery depend on yarn structure, fabric construction, finishing, and garment design, so trials should be completed before bulk production.
What are the benefits of PBT/PET yarn?
PBT/PET yarn can provide a combination of elasticity, resilience, dimensional stability, and polyester processing characteristics. It may be useful in stretch fabrics where the buyer wants controlled recovery and a specific hand feel.
Where can moisture-wicking DTY be used?
Moisture-wicking DTY can be considered for sportswear, base layers, uniforms, travel clothing, active casualwear, and warm-weather garments. Moisture management depends on yarn, fabric structure, finishing, and testing conditions.
Does antibacterial yarn remain effective after washing?
Durability depends on the antibacterial technology, active material, yarn structure, fabric construction, and washing conditions. Customers should request durability test results based on the intended application and claim requirements.
Can flame-retardant DTY guarantee that a finished garment is flame resistant?
No. Flame performance must be evaluated on the finished fabric or garment under the relevant standard. Yarn type is only one factor; fabric weight, construction, blends, finishing, seams, and washing can all affect the result.
Can the company develop a custom DTY specification?
The product information states that orders for different kinds of differentiated yarn can be accepted. Customers should provide detailed requirements concerning end use, denier, filament count, luster, function, elasticity, color, fabric construction, and required certifications.
What should be tested before placing a bulk order?
The buyer should test knitting or weaving performance, breakage, tension, dye uptake, color fastness, fabric appearance, dimensional stability, pilling, stretch and recovery where relevant, and any functional claims required for the final product.
Conclusion
The presented DTY yarn portfolio is designed for a textile market that increasingly values sustainability, functional performance, product differentiation, and manufacturing reliability. It covers conventional polyester yarn for stable mainstream production, recycled DTY for lower-impact product development, cationic-dyeable yarn for special coloration, high-elastic and PBT/PET products for stretch applications, and functional yarns for moisture management, antibacterial performance, flame retardancy, warmth, and cotton-like comfort.
Its competitive strength lies in the combination of product breadth, detailed denier and filament-count choices, differentiated functions, and an application-oriented development approach. Instead of offering only one general-purpose polyester yarn, the range gives fabric mills and brands multiple pathways to create fabrics with distinct visual, tactile, environmental, and performance characteristics.
Advanced DTY manufacturing requires more than texturing equipment. It depends on feedstock control, stable spinning, precise drawing, carefully managed false-twist texturing, proper intermingling, high-quality winding, thorough inspection, and responsive technical support. The company’s focus on recycled yarn, functional yarn, research cooperation, international service, and customized differentiation indicates a manufacturing model intended to support both standard orders and specialized development projects.
For buyers, the most effective approach is to define the desired finished-fabric performance first and then select the appropriate yarn family, luster, denier, filament count, and functional platform. With proper sampling and technical validation, the product range can support applications from everyday knitwear and home textiles to activewear, protective clothing, high-elastic garments, and sustainability-driven textile collections.
References
1. Product specification information for recycled, normal, cationic-dyeable, high-elastic, functional, cotton-like, hollow warm, and Acy DTY yarns supplied in the source materials.
2. General principles of polyester filament spinning, drawing, false-twist texturing, intermingling, winding, and yarn quality inspection.
3. General textile testing practices for linear density, tensile properties, elongation, crimp, shrinkage, evenness, color fastness, moisture management, antibacterial performance, and flame behavior.
4. General industry guidance concerning recycled polyester, recycled-content documentation, responsible material selection, and textile product traceability.
5. General technical considerations for fabric development using semi-dull, full-dull, cationic-dyeable, high-elastic, PBT/PET, moisture-wicking, antibacterial, flame-retardant, cotton-like, and hollow warm yarns.
Product: General diagram of DTY except colored silk
Popular products
-
Premium Cationic Interlock Stretch Comfort Fabric
-
Moisture-Wicking Nylon Woven Fabric
-
Double-faced jacquard elastic fabric
-
Heather Grey Double-faced cationic jersey fabric
-
Anti-static Cationic Knitted Rib Fabric
-
High-Stretch Cationic Jersey Fabric
-
High Quality Cationic DTY Spandex Two Sides Brush Dralon Knit Fabric for Garment Thermal Underwear
-
Durable Anti-Pilling Knitted Fabric for Home Textiles
-
Wash-Resistant Cationic Elastic Knitted Fabric for Garment Industry
-
Breathable Double-Faced Elastic Composite Fabric
-
-
-
- whatsapp:
- 0086-13962559622
-
- skype:
- skype.aliceshenghong
-
- Wechat:
COPYRIGHT © 2016 Suzhou Junhui Textile Co., Ltd.